Bulk CNC Machining for Efficient High Volume Production
2026-10-08
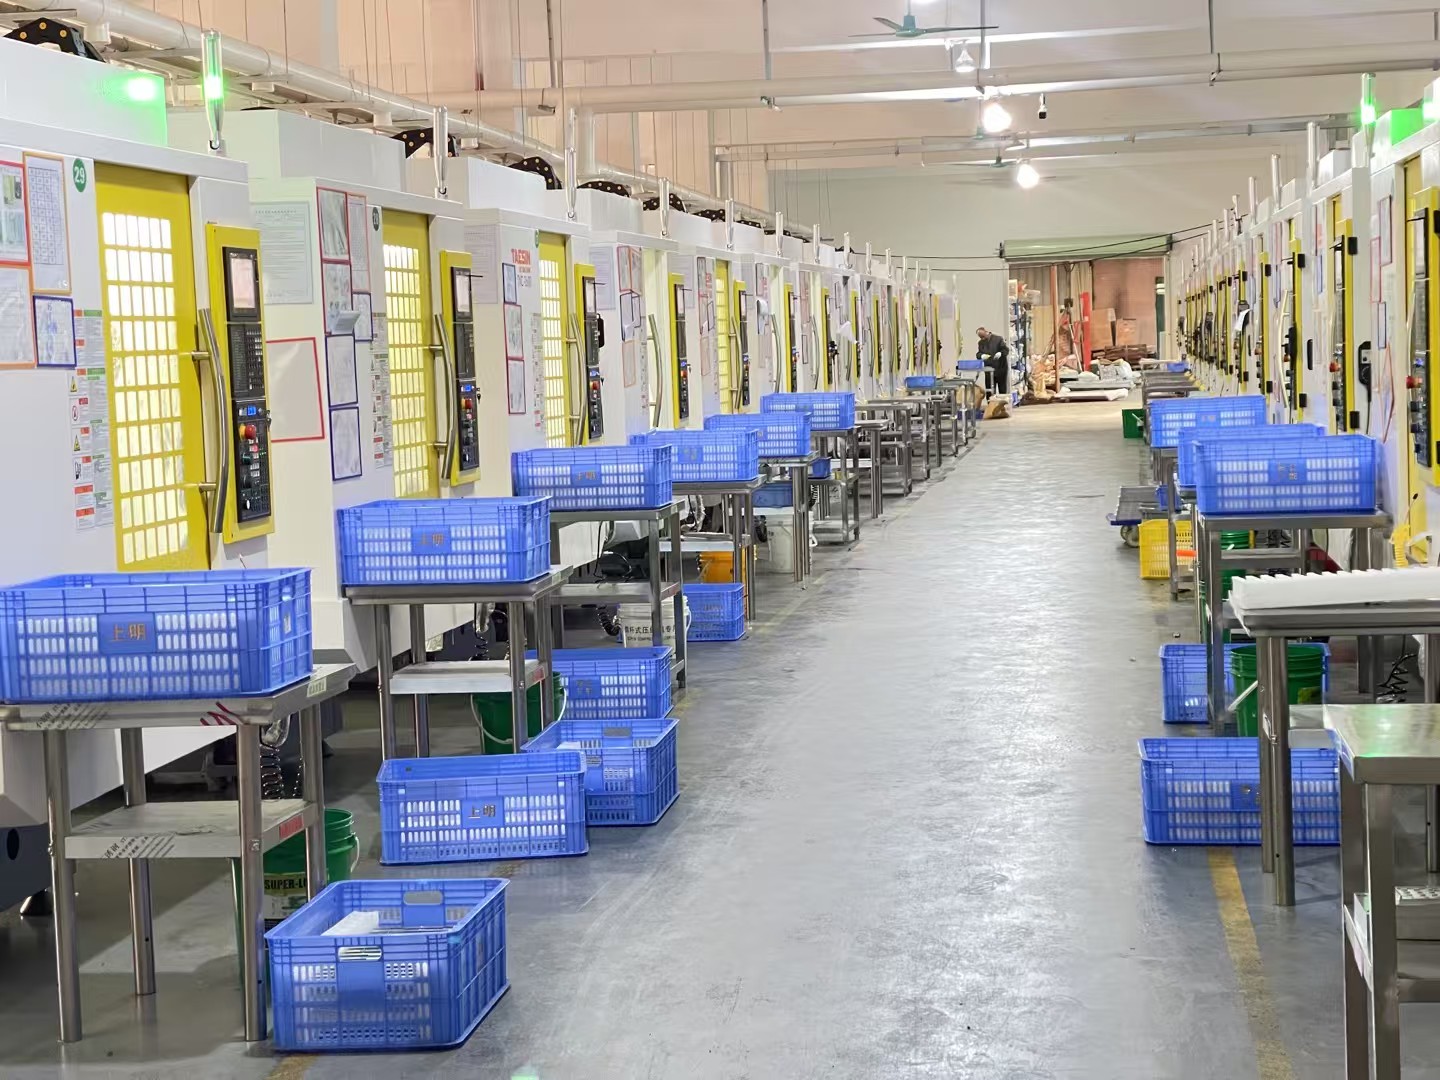
Scaling production often exposes hidden inefficiencies—excess setups, tool changes that eat into cycle time, and tolerances that drift when machines run hot. Bulk CNC machining flips that script, provided the process is engineered for volume, not just speed. At Peak Fasten, we treat high-volume runs as a system: optimizing fixtures, feeds, and toolpaths so output climbs without sacrificing repeatability. So what actually separates a chaotic parts flood from a lean, predictable pipeline? The answer lies in a few overlooked details.
Scaling Volume Without Losing Your Grip on Tolerance
When you push a process from prototype volumes into full production, tolerance drift rarely comes from a single dramatic failure. It sneaks in through smaller shifts: a new operator sets a fixture slightly differently, tooling from a second supplier cuts a few microns off, or a multi-cavity mold starts showing cavity-to-cavity variation that was invisible at ten parts per day. Too many teams try to fix these issues by just chasing the spec limits after the fact, which only adds inspection burden and scrap without addressing the root cause.
The real work happens before the volume curve goes upward. You need a baseline process capability that holds across different shifts, material lots, and equipment states, not just a golden batch that passed first article. That often means mapping how each input variable affects the critical dimensions and then locking down the ones that matter most. In practice, a well-placed automated gauge that feeds measurement data back to the machine control can prevent a small thermal drift from turning into a weekend of quarantined parts. It is far cheaper to adjust for tool wear every few hundred cycles than to discover a full day of output is out of tolerance.
Management also has to change its reflexes. If the only number reviewed in the morning meeting is units shipped, tolerance problems will always be someone else's surprise. Instead, track capability indices and scrap trends right next to output, and give operators the authority to pause a run when something looks unstable. Scaling volume without losing your grip on tolerance is less about heroic inspection and more about designing a process that stays boringly predictable as the numbers climb.
Material Decisions That Keep a Long Run Smooth
Fabric choices make or break a long run before the first mile is even logged. A shirt that soaks through by mile four turns into a cold, heavy second skin, while a blend with merino or high-gauge polyester moves sweat off your back and dries while you're still in motion. Seams get less attention but cause more damage: flatlock stitching and bonded panels remove the tiny ridges that rub raw after two hours. When every mile repeats the same arm swing, a badly placed seam becomes a slow burn you can't ignore.
Shoes absorb more punishment than any other piece of kit, but the midsole foam is only half the story. Outsoles with dual-density rubber and wider lug patterns keep grip on loose gravel without turning into dead weight on pavement. The upper matters just as much—engineered mesh with reinforced overlays holds the foot without pinching when feet swell. Skip the flashy knit that looks fast on a shelf but stretches into a sloppy fit by mile fifteen. Durability in materials isn't boring; it's the difference between a run that ends at your door and one that ends in a limp.
Accessories quietly decide comfort. A hydration vest with coarse nylon straps soaks up sweat and salt, then grinds against collarbones for the last ten miles. Swap to perforated foam and silicone-backed webbing and the load stays put without friction. Even socks follow the rule: cotton hides moisture where blisters start, but a thin wool-synthetic wrap dries fast and keeps toes moving independently. The right materials don't promise speed. They promise that nothing hurts at mile eighteen, and that's what keeps the run smooth.
Automation Isn't Just a Robot Loading Parts
When people picture automation, they often imagine a robotic arm picking up a metal component and placing it into a CNC machine. That image is accurate but incomplete. Automation extends far beyond physical motion—it lives in the software that schedules jobs, the sensors that predict tool wear, and the data pipelines that adjust production parameters without a human ever touching a keyboard. Limiting your understanding of automation to a robot loading parts means ignoring the majority of what actually keeps modern manufacturing running smoothly.
Consider the quiet work happening before a single part is ever machined. Automated quoting tools analyze CAD files and generate accurate estimates in seconds. Inventory systems track raw material levels and automatically reorder stock when thresholds are crossed. Even the inspection process has moved beyond manual calipers—vision systems and coordinate measuring machines now verify dimensions and surface finish while flagging anomalies in real time. None of these tasks involve a robot arm, yet all of them reduce lead times, cut waste, and free skilled workers to focus on problems that genuinely require human judgment.
The real power comes from connecting these invisible layers. A sensor detects slight vibration in a spindle, the control system adjusts feed rates on the fly, and a maintenance ticket is generated before a failure occurs. Meanwhile, the production schedule shifts automatically to accommodate the adjusted cycle time, and the customer receives an updated delivery estimate—all without anyone picking up a phone. That is the true face of automation: a coordinated flow of information and decisions, where a robot loading parts is just one visible actor in a much larger, smarter system.
Fixture and Setup Choices That Compound Throughput
The first overlooked detail is how much play exists in the locating surfaces. A few microns of slop in a pin or a slight bow in a baseplate rarely shows up as a scrapped part on day one. Instead, it forces the toolpath to compensate in ways that are invisible in simulation. You slow the feed override to quiet a harmonic. You add a spring pass to chase a dimension that drifted after clamping. Each adjustment seems rational in isolation, but across a shift they stack into extra minutes per cycle that nobody tracks as a line item.
A more deliberate setup strategy treats every contact point as a load path. Switching from three-point to six-point location for a flimsy bracket might only gain two seconds of roughing time, but it also removes the need to re-tighten mid-run or babysit a dial indicator. Quick-change pallets with repeatable zero points let an operator swap fixtures without re-probing, which sounds like a convenience until you realize the machine no longer sits idle while someone nudges a vise back into square. Those recovered minutes then absorb the inevitable hiccup—a dull insert, a coolant nozzle knocked out of position—without the whole cell falling behind.
The difference shows up in the cumulative behavior, not the spec sheet. Two shops can run identical machines and similar parts, yet one consistently ships more because its fixturing tolerates minor variation instead of demanding constant correction. It's not a single heroic upgrade. It's the daily elimination of tiny, energy-sapping adjustments that would otherwise eat the margin between quoted cycle time and actual throughput.
In-Process Checks That Don't Put the Line to Sleep
Some inspection stations slow down throughput because every unit must pause under a camera or probe. The better approach is to design checks that happen while the line keeps moving, using sensors and vision systems that capture data on the fly. This means parts are measured, read, or verified without ever stopping the conveyor or robotic cell. The result is a smoother cadence, fewer bottlenecks, and less wear on indexing mechanisms that would otherwise start and stop constantly.
A practical example is a laser profilometer mounted over a moving rail. As each assembly passes beneath, the sensor takes hundreds of cross-section samples and compares them to a golden reference. If a feature drifts out of tolerance, the system flags that specific unit for a downstream divert, but the rest of the line never hesitates. The same logic applies to barcode reading with high-speed imagers, RFID tag verification, or even non-contact torque checks on rotating shafts. The key is that the check adds no additional cycle time because it piggybacks on motion that already exists.
Engineers often worry that inline, non-stop inspection sacrifices accuracy. In reality, modern algorithms compensate for motion blur, vibration, and lighting changes, so repeatability can match or beat static checks. The real trick is choosing sensor placement and triggering so that the measurement window aligns with a stable portion of the travel path. Once that alignment is locked in, you get continuous quality data without ever asking the line to take a nap.
Why Cost Per Part Starts Before the First Cut
Most shops blame machining time for high part costs, but the real damage is usually done long before a cutter touches material. The chosen stock size, material grade, and even the way a part is dimensioned on the drawing lock in expenses that no amount of spindle speed can claw back. Once the blank is loaded and the program starts, those early decisions have already set the floor for cycle time and scrap risk.
Take a simple bracket. If the designer calls for an unnecessarily tight bore tolerance, the machinist may need to slow the feed, add a finish pass, or switch to a more expensive tool. If the blank comes as a solid block instead of a near-net casting, someone has to pay for all that extra chip removal and the tool wear that comes with it. These aren't cutting problems—they're planning problems. Yet they hide in plain sight until the job is already running behind.
The shops that consistently hit low cost per part treat the pre-cut phase as the real battleground. They challenge tolerances, suggest small geometry changes, and standardize features before the CAM work begins. A ten-minute conversation with a customer about a non-functional surface can save more than a full day of machining optimization. The first cut doesn't create the cost; it just reveals the choices already made.
FAQ
Bulk CNC machining focuses on producing large quantities of identical or similar parts, often using optimized setups, automated loading, and dedicated fixturing. Unlike one-off jobs, the process is tuned for repeatability and speed, so every cycle yields parts that match the original design with minimal human intervention.
Automotive, medical device, aerospace, consumer electronics, and industrial equipment manufacturers rely heavily on bulk CNC machining. Any sector needing thousands of consistent, tight-tolerance components—from surgical instruments to connector housings—can reduce unit costs and lead times through volume production.
By spreading setup and programming expenses across a large batch, each part absorbs only a small fraction of those fixed costs. Additionally, optimized tool paths, faster cycle times, and less scrap mean material and labor costs per unit drop significantly compared to low-volume runs.
Aluminum, stainless steel, brass, titanium, and engineering plastics like PEEK, Delrin, and nylon are all suitable. The choice depends on mechanical requirements, thermal resistance, and weight targets, but the process itself remains consistent across most machinable metals and polymers.
It starts with robust fixturing and tool condition monitoring. Frequent in-process inspection, combined with automated probing and statistical process control, catches drift early. Many shops also use temperature-controlled environments and high-quality carbide tooling to keep dimensional variation within a few microns.
While prototypes are usually low quantity, bulk CNC works well for final parts and bridge tooling. However, if you need a few thousand parts before committing to injection molding, CNC offers design flexibility and faster turnaround without the upfront cost of a mold.
Designing with standard tool sizes, avoiding deep pockets with small radii, and minimizing unnecessary tight tolerances can speed up machining. Keeping wall thickness uniform and grouping features for fewer setups also reduces cycle time and helps keep the process stable over long runs.
Conclusion
High-volume CNC work isn't about running the same program faster; it's about removing every small delay and variation that compounds across thousands of parts. Holding tight tolerances at scale means designing processes so that thermal drift, tool wear, and fixture flex don't drift into scrap. Material choice matters long before the spindle starts—picking a grade that machines consistently, chips predictably, and doesn't chew through inserts keeps a long run from turning into a fire drill. And while a robot arm looks impressive, real automation starts with things like automatic tool setting, pallet changers, and workflow that lets one operator manage multiple machines without babysitting each cycle.
Fixtures and setups often decide whether you're competitive or just busy. Quick-change pallets, zero-point clamping, and locating features that repeat within microns can double throughput without touching cutting speeds. In-process checks need to be quick and meaningful—probing critical dimensions every Nth part or using tool monitoring to catch breakage before it ruins a batch—so the line never stops for hours of offline inspection. True cost per part is set before the first cut: by programming efficient toolpaths, staging materials, and thinking about chip evacuation. When all these pieces work together, bulk CNC machining stops being a series of machines and starts acting like a production system.
Contact Us
Contact Person: Mason Lv
Email: [email protected]
Tel/WhatsApp: +86 13027998452
Website: https://www.peakfastentech.com