China Sewer Jetting Machines Factory: How Advanced Manufacturing Meets Global Standards
2026-09-18
When you think of industrial-grade sewer jetting machines, China might not be the first place that comes to mind—but the team at AMJET is quietly rewriting that story. Blending advanced manufacturing with rigorous global standards, this factory turns out equipment that rivals the best in the world, yet many buyers still don’t know how they pull it off. Here’s a closer look at the precision, innovation, and quality control behind every machine.
Inside the Automated Assembly Floor
The floor doesn't hum so much as breathe—a low, synchronized pulse of servos and belt drives. Rows of six-axis arms work in staggered rhythm, each completing a weld, a fastener, a micro-adjustment before handing the chassis to the next cell. Overhead gantries glide on magnetic tracks, ferrying subassemblies to stations that recalibrate themselves between cycles. It's less a production line than a tightly choreographed relay, where every motion is measured in milliseconds and every handoff is verified by laser.
What stands out at eye level is the absence of clutter. Cables vanish into cable trays, tool changers dock with a click, and floor markings guide autonomous carts that reroute around obstacles without slowing the pace. Vision systems blink from above, checking torque angles and surface finishes with the kind of obsession a human inspector might show on a first morning shift. Yet there are still people here—fewer than you'd expect, but positioned at decision points, watching dashboards that turn machine data into a live map of the line's health.
How Every Machine Earns Its Certification
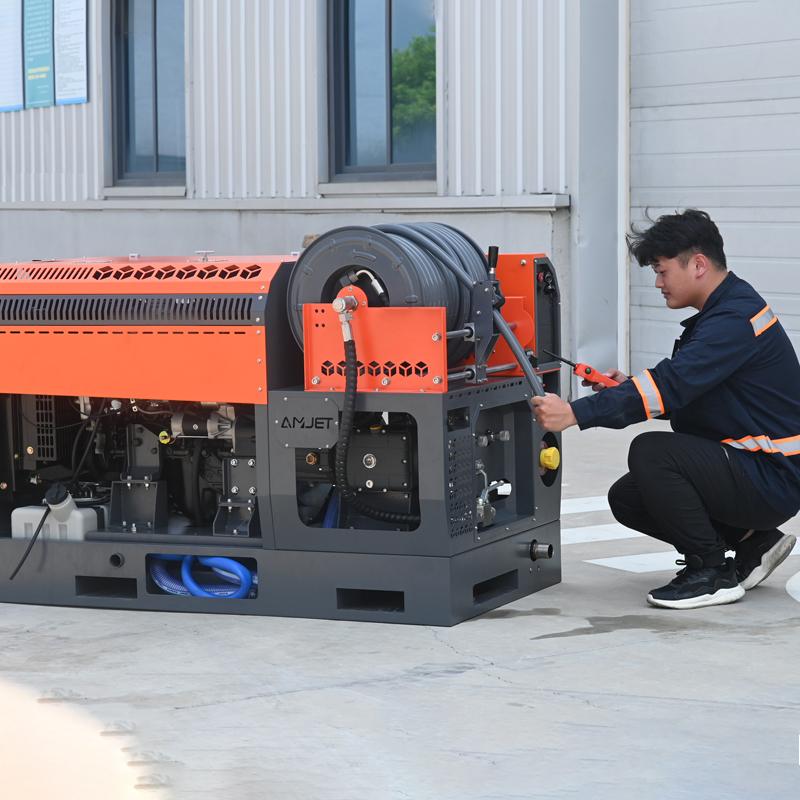
Before a machine can be shipped to a customer, it has to prove itself in ways most people never see. The certification process starts with a teardown inspection, where every weld, seal, and electrical connection is checked against a thick binder of engineering drawings. Then the machine is bolted to a test rig and pushed through load cycles that mimic ten years of abuse in a single week. Sensors record every twitch, and if a bearing runs just a few degrees too hot, the whole unit gets pulled off the line.
Not every machine makes it on the first try. Some fail during the cold-start test, when the hydraulic fluid is thick as honey and the motor has to drag itself awake. Others trip a safety interlock during the emergency-stop drill, which means a redesign, not just a tweak. The ones that pass are issued a certificate that's tied to the machine's serial number, not the model. That way, the piece of paper actually means something—it refers to this exact unit, with its own quirks and test logs, not a batch of identical siblings.
Material Choices That Survive Harsh Sewers
High-density polyethylene (HDPE) remains a workhorse in corrosive sewer environments because it shrugs off hydrogen sulfide, sulfuric acid, and the constant abrasion from grit. Unlike concrete or ductile iron, HDPE does not rely on a passive oxide layer or alkaline buffer; its molecular structure resists chemical attack even at low pH. Welded joints eliminate the gasket and bell failures that often plague rigid pipe under shifting soil loads, which is why trenchless installers favor it for slip-lining and pipe bursting in aggressive ground.
Vitrified clay pipe, though older than most alternatives, still outperforms plastics in one key area: resistance to high-temperature discharges and rodent gnawing. The glass-like surface resists slime buildup and sulfuric acid produced by thiobacillus bacteria. For manholes and wet wells, a calcium aluminate cement or epoxy lining over precast concrete buys time, but the real improvement comes from using polymer concrete or fiberglass-reinforced plastic for the structure itself. Stainless steel alloys such as 316L should be reserved for fasteners, weirs, and pump rails; using them for entire pipelines is rarely cost-effective unless chloride levels are extreme.
Tailoring Pressure and Flow for Export Clients
Export buyers rarely run systems the same way domestic customers do. A line that works at 6 bar in one region may need 8 bar or far lower flow tolerance elsewhere, depending on local pipe sizing, altitude, and even the additives blended into process water. We start by confirming the actual operating window on-site, not the assumed one from a datasheet, then map pressure curves to the client's worst-case inlet conditions rather than a clean-room benchmark.
That same logic applies to flow control. Instead of shipping a one-size-fits-all orifice or valve assembly, we adjust internal clearances, impeller trim, or bypass settings so the unit arrives ready for the destination's typical viscosity and temperature swing. Where local service access is limited, we also simplify adjustment points and mark them with bilingual torque specs, cutting the chance of a well-meaning tweak turning into a warranty claim.
In-House Testing That Mimics Real Job Sites
We don't just test gear in a sterile lab. Our in-house testing grounds are built to replicate the unpredictable conditions of actual job sites—uneven terrain, overhead obstacles, mud, dust, and tight access points. That means hydraulic systems get pushed on slopes, engines run in heat and cold, and attachments are cycled under the same repetitive stress they'd see on a long workday. By the time a machine leaves our facility, it's already survived a week of simulated abuse that many units won't see in a year.
Every station in our test yard mirrors a specific real-world scenario. A concrete pad with buried conduits checks for vibration transfer and ground pressure. A compacted gravel loop with sharp turns tests steering response and tire wear at full load. We even have a mud pit with variable depth to stress seals and filtration under constant contamination. Operators run machines through these courses while data loggers capture temperature, pressure, and cycle counts. If a component flags early, we tear it down and adjust before production.
What sets this apart is the feedback loop. Test operators file daily reports that go straight to engineering, not a marketing folder. A cracked weld on a ROPS mount, a hose chafing against a frame rail, an unexpected hydraulic lag on cold mornings—these details drive immediate revisions. We'd rather find the weak point in our yard than have a customer find it on their site. That's the entire point of building a test environment that feels like a job site without the safety waivers.
Documented Parts, Proven Origins
Each component that goes into our products carries a paper trail that would satisfy the most detail-obsessed engineer. We don't just say a part is good—we can show you the mill certificate, the batch number, and the test report that came with it. From the first pour of molten metal to the final torque check, every step is logged and cross-referenced.
The supply chain behind these parts isn't a black box. Every supplier we use has been visited, audited, and re-audited over multiple production cycles. If a bearing comes from Osaka or a casting from a foundry in Northern Italy, that origin isn't a marketing line—it's a documented fact you can verify with the serial number stamped on the part itself.
This level of traceability means fewer surprises down the road. When a part behaves exactly as its documentation says it will, you spend less time troubleshooting and more time building. And if a question ever comes up, the answer is already in the file, not buried in someone's memory.
FAQ
The facility relies on automated laser cutting and robotic welding to keep frame tolerances tight, then runs each unit through a multi-stage pressure test that simulates a fully blocked drain line. That combination cuts down on weld fatigue and lets them catch seal leaks before shipping, which is something smaller shops often skip.
They align with CE and ISO 9001 requirements as a baseline, with certain high-pressure pumps also carrying UL or CSA approvals depending on the destination market. Third-party inspectors are invited for batch audits, and every machine ships with a traceable test report tied to its serial number.
Rather than offering only fixed configurations, the engineering team works from a modular chassis platform. Buyers can request different tank sizes, hose reel positions, or engine choices, and the factory produces a layout drawing for approval before assembly begins. That avoids expensive rework after the unit arrives.
Each unit is tested with water at 10 to 15 percent above its rated working pressure, and the nozzle is run through a clear pipe rig to confirm jetting angle and forward pull. For cold-climate orders, they also run a freeze-protection cycle to make sure residual water drains properly from the pump and valve block.
The factory keeps a digital service portal with exploded parts diagrams and torque specs, and they stock wear parts in regional warehouses in Europe and North America. Video calls with a bilingual engineer are available for troubleshooting, and major components are designed to be swapped with basic hand tools.
It is a mix. The structural steel, tanks, and hose reels are produced in-house, while high-cycle components like pumps, engines, and control valves come from established suppliers in Italy, Germany, or Japan. That gives buyers familiar service networks for the parts that matter most.
A serialized dossier includes weld inspection notes, pump flow and pressure curves, electrical continuity checks, and a signed final test sheet. Photos of the unit during assembly are attached, so the buyer can see exactly which fittings and routing were used on their specific order.
Conclusion
Walk the factory floor and you'll see why consistency matters. Automated assembly stations align pumps, gearboxes, and chassis rails, while torque tools record every fastener setting in real time. Certification isn't a rubber stamp here; each completed machine passes a multi-point audit covering pressure integrity, electrical grounding, and control-system response before it is allowed to wear the compliance plate. Materials are chosen for longevity in the worst conditions, not just for cost: heat-treated stainless nozzles resist erosion, hoses are reinforced to withstand abrasive grit, and frames get a double-layer coating against corrosion. When an export order comes in, engineers adjust pump displacement, nozzle orifice size, and unloader settings to match the client's actual pipe networks and pressure norms, so a unit built for Northern Europe performs differently from one headed to Southeast Asia.
The test bay is where theory meets reality. Instead of a quick run on a bench, machines are hooked to vertical risers, long hose reels, and dirty-water recirculation tanks that simulate the blockages and backpressure of a live sewer line. Every seal, valve, and gauge is watched for the smallest deviation. Traceability runs deep: each pump serial, hose batch, and frame weld carries documentation that links back to its material certificate and production date. That level of record-keeping, combined with automated assembly and job-site-style validation, is what lets a Chinese factory deliver sewer jetters that meet buyer expectations in Europe, the Americas, and beyond without excuses.
Contact Us
Contact Person: Mike
Email: [email protected]
Tel/WhatsApp: +86 19545555505
Website: https://www.amjeting.com/