EMI Filter Factory: Inside Precision Manufacturing for Superior Noise Suppression
2026-10-14
Step inside an EMI filter factory, and you'll quickly realize that noise suppression isn't just a checkbox on a spec sheet—it's a craft. From tightly wound toroids to precisely layered PCBs, every component is engineered to tame interference that can cripple sensitive electronics. At DOREXS, this obsession with precision isn't marketing fluff; it's built into the factory floor, where automated winding, hi-pot testing, and thermal cycling separate rugged filters from fragile imitations. Curious what separates a truly superior EMI filter from the rest? Keep reading.
Core Material Decisions That Shape Attenuation Curves
Material selection sets the baseline for how energy is dissipated across a frequency range. Open-cell foams, for instance, rely on tortuous air passages and viscous boundary layers to convert acoustic energy into heat, giving a relatively smooth, broadband attenuation curve. By contrast, dense viscoelastic sheets and fibrous mats tend to show more pronounced low-frequency roll-off, with the curve's slope tied closely to fiber diameter distribution and packing density.
Thickness and density are not interchangeable levers; they push the curve in different directions. Adding thickness tends to shift effective attenuation toward lower frequencies, while increasing density can raise mid- and high-frequency losses but may reflect more energy if the surface becomes too compact. A practical workaround is to combine a lightweight absorber with a thin mass layer, which alters the curve's knee point without imposing a heavy penalty on overall weight.
Composite treatments introduce deliberate peaks and notches into the attenuation curve. Bonding a perforated panel over a porous core, for example, creates a Helmholtz-type resonance that boosts absorption in a narrow band—useful when a specific tonal noise needs to be suppressed. Tuning hole diameter, spacing, and air gap depth reshapes that peak's position and width, turning material choice into a direct control on the curve's shape rather than a fixed property of the base material.
Precision Winding Tension and Turn Spacing
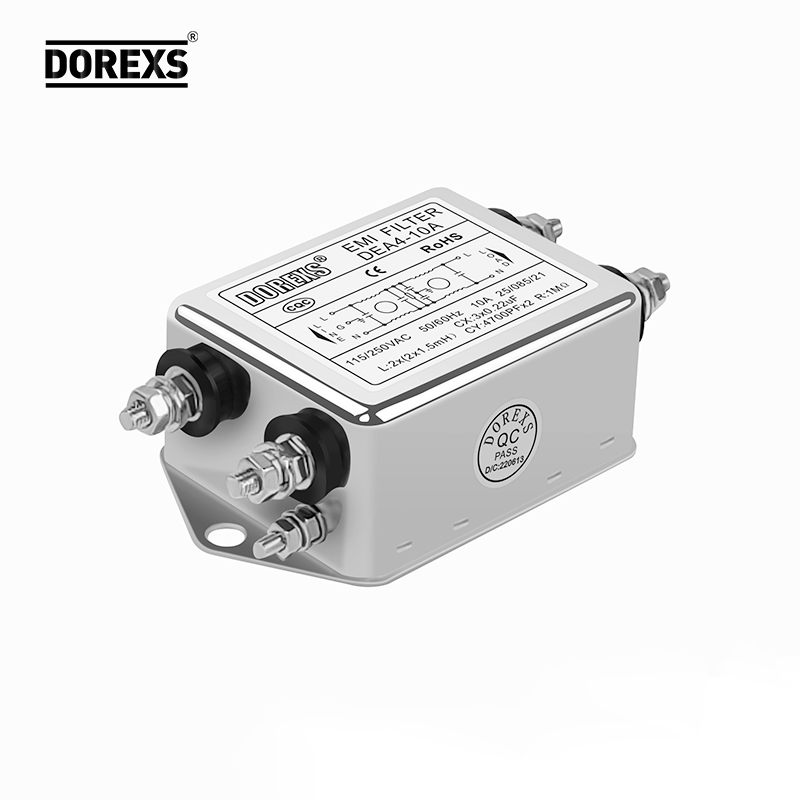
Maintaining consistent wire tension during winding is critical for achieving uniform layer compaction and repeatable coil dimensions. Too little tension allows the wire to shift or bulge, creating voids that alter inductance and increase vibration sensitivity, while excessive tension can stretch the conductor, raise its resistance, and even damage thin insulation. Precision systems typically employ closed-loop tensioners with dancer arms or electronic feedback to hold tension within a narrow band, compensating for spool inertia and speed changes.
Turn spacing, the gap between adjacent wires in a layer, directly affects distributed capacitance and thermal behavior. Irregular spacing produces localized electric field concentrations that can lead to partial discharge in high-voltage designs or unpredictable high-frequency losses. Automated winding machines use high-resolution encoders and vision systems to monitor edge-to-edge placement, adjusting traverse speed and guide position on the fly to maintain spacing accuracy down to a few micrometers.
The interaction between tension and spacing is particularly important in multilayer coils and fine-wire applications. A sudden tension spike can pull a previous turn out of position, creating a spacing defect that propagates through subsequent layers. Advanced controllers therefore coordinate both parameters using model-based algorithms that anticipate wire behavior around corners and over uneven substrates, ensuring that every turn lands with the same pitch and residual stress.
Automated Soldering With Manual Touch-Ups for Critical Joints
Fully automated soldering lines handle the bulk of board work with impressive repeatability, but they still struggle when a joint carries more thermal mass than the surrounding parts. Ground planes, heavy connectors, and shielded cans pull heat away from the pad faster than the preheat profile can compensate. In those spots, the solder might wet unevenly or form a grainy fillet that passes initial inspection only to fail later under vibration or thermal cycling.
That is where a trained operator steps in with a fine-tip iron and a controlled amount of additional flux. Rather than reflowing the entire assembly or pushing the oven hotter—both of which risk disturbing nearby components—the operator touches up only the joints that show marginal wetting, dull finish, or incomplete barrel fill. The decision to intervene is usually based on visual criteria plus a quick resistance or pull test on a sample basis, not on blanket rework of every similar joint.
Keeping this hybrid approach consistent means documenting which joints typically need manual attention and feeding that information back into stencil design, pad geometry, or solder paste volume. Over time, the number of manual touch-ups should drop as the automated process adapts, but a zero-touch-up target is usually unrealistic for boards with mixed thermal demands. The goal is not to replace automation with handwork, but to use handwork where it adds the most reliability without slowing the line more than necessary.
Real-Time Spectrum Analysis During Final Assembly
Bringing real-time spectrum analysis onto the final assembly line changes how engineers catch signal anomalies before a unit ships. Instead of relying on spot checks or off-line troubleshooting, each device gets a full spectral sweep while still in its assembly fixture. This immediate feedback reveals spurious emissions, clock harmonics, or poorly seated connectors that might otherwise pass basic functional tests. The result is a tighter feedback loop between assembly errors and RF performance, reducing the number of units that reach final QA with hidden issues.
The practical value shows up in complex builds where multiple radios, antennas, and high-speed digital buses share limited space. A real-time analyzer can flag subtle interference patterns that only appear when several subsystems run at once. For example, a slight misalignment in a shield can let a switching regulator’s noise leak into a sensitive receiver band. Catching this during assembly means a technician can reseat the shield or adjust a cable route in seconds, rather than sending the unit back from field test weeks later.
To get the most from this approach, assembly stations need a spectrum view that is updated fast enough for line operators, not just RF engineers. Modern systems overlay pass/fail masks directly on the live trace, so a worker sees a green or red condition without interpreting dBm plots. This keeps the line moving while still enforcing strict spectral compliance. Over time, the collected traces become a valuable dataset for spotting recurring assembly defects tied to specific batches or operator shifts.
Custom Enclosure Designs for Odd-Form Factor Boards
Odd-form boards rarely fit into anything you can buy off the shelf. The mounting points are never where you expect them, and one board might have three different connectors sticking out on all four sides. Building a custom enclosure around the actual board layout eliminates the guesswork and prevents the board from flexing or shorting against a badly matched case. It also means you can place cutouts exactly where cables need to enter, instead of relying on oversized knockouts that let dust and debris inside.
Before committing to a final material, make a quick mock-up from cardboard or thin acrylic. It costs almost nothing and will reveal clearance problems that are invisible in CAD, like a tall capacitor that blocks the lid or a USB port that sits 2 mm lower than you thought. Once the dimensions feel right, print a test shell in PLA or PETG, but leave 0.3 mm to 0.5 mm of slack around every connector opening. Too tight, and you'll crack the housing or scrape the board during insertion; too loose, and the board will rattle when the device is moved.
For production runs or boards that run hot, consider moving beyond basic 3D printing. Nylon and ASA prints hold up better under heat and repeated handling, while CNC-machined aluminum gives you both shielding and a proper heat sink if you add a thermal pad between the board and the case wall. Include a few internal standoffs or ribs to keep the board level, and design the enclosure so the PCB slides in from one end rather than being dropped in from above. That small change makes assembly and field repairs much less frustrating.
Batch-Level Thermal Cycling and Burn-In Protocols
Accelerated stress testing at the batch level serves as a critical gate before volume shipment. Instead of relying on a small sample from a single wafer, these protocols pull units from multiple lots and assembly dates, subjecting them to repeated temperature excursions between -40°C and +125°C. The ramp rates and dwell times are intentionally aggressive, exposing weaknesses in solder joints, die attach materials, and package interfaces that would otherwise remain dormant until field deployment.
Burn-in complements thermal cycling by combining elevated temperature with dynamic electrical bias. Devices are operated near their maximum rated voltage while ambient temperature is held at or above 125°C for 48 to 168 hours. This combination drives ion migration, oxide breakdown, and early-life defect acceleration. Batch-level tracking means every unit is serialized and tied to its specific assembly lot, allowing engineers to identify which process window introduced marginal parts before they escape into the supply chain.
Tightening these protocols requires careful attention to thermal uniformity across the chamber and consistent monitoring of power supply stability. Variations in airflow or rack position can create false failures or, worse, let weak units pass. Many teams are now shifting to per-part temperature sensing and adaptive burn-in profiles, where the stress level is adjusted based on real-time leakage current measurements. This not only improves defect detection but also reduces overall test time by focusing thermal stress where it is most likely to reveal latent reliability risks.
FAQ
Every coil is wound to tight inductance tolerances, usually with automated tension control to avoid micro-fractures that would later show up as attenuation dips under load.
Nanocrystalline cores hold permeability better at high temperatures and offer higher saturation flux density, which keeps common-mode chokes compact without sacrificing low-frequency noise suppression.
Each unit goes through a vector network analyzer test across the target frequency band, and batch samples are additionally checked for insulation resistance, leakage current, and thermal cycling drift.
High-end builds pay close attention to parasitic coupling: input and output leads are routed apart, ground planes are kept continuous, and component placement follows a shielding-first approach rather than pure density.
The potting compound affects both thermal dissipation and parasitic capacitance. A poorly chosen resin can shift the filter's resonance point and actually worsen high-frequency noise leakage.
Yes, by adjusting the filter's source and load impedance assumptions, selecting different capacitor values and damping networks, and re-optimizing the insertion loss curve for the specific application rather than a generic 50-ohm system.
Laser marking creates durable, high-contrast part numbers and ratings without using inks or labels that could outgas, peel, or compromise the filter's surface insulation in harsh environments.
They use selective soldering or reflow ovens with tightly profiled thermal zones, then run X-ray inspection on a sample basis to catch voids or cold joints that could crack under vibration and break the ground path.
Conclusion
The attenuation curve of any EMI filter begins long before the first component is placed, with core material choices that set the baseline for impedance across frequency. Ferrite cores dominate for common-mode suppression, but when a design calls for sharp roll-off at lower frequencies, nanocrystalline or amorphous cores come into play, each shifting the knee of the curve in ways that datasheets alone rarely capture. On the winding floor, tension is not just a machine setting; operators adjust it in real time to avoid stretching fine wire or introducing inconsistent turn spacing. Even a half-millimeter drift in spacing can add enough parasitic capacitance to compromise high-frequency rejection, so the work relies as much on trained hands as on automated spindles.
Once the windings are finished, automated soldering ensures repeatable joint quality, but certain critical connections still get a manual touch-up where solder fillets need to be inspected under magnification. Final assembly is where the filters meet a real-time spectrum analyzer, allowing technicians to watch insertion loss curves on screen and immediately spot any resonance or leakage that should not be there. Odd-form factor boards receive custom enclosures, designed not only to fit but also to maintain shielding integrity with proper grounding tabs. Before shipping, every batch goes through thermal cycling and burn-in, pushing the filters through temperature swings while under load to expose latent weaknesses that would otherwise appear only in the field.
Contact Us
Contact Person: Eric
Email: [email protected]
Tel/WhatsApp: 8618117837140
Website: https://www.emcdorexs.com