Top Beverage Production Line Manufacturer: How to Choose the Right Partner for Your Bottling Facility
2026-10-01
Choosing the right beverage production line manufacturer can make or break your bottling facility’s efficiency, output quality, and long-term ROI. From filling precision to hygiene compliance, every component matters—and the wrong partner often hides costly compromises. That’s where INTOP Machinery comes into focus. In this guide, we’ll break down what truly separates a dependable bottling line builder from the rest, so you can invest with confidence.
Look Beyond the Spec Sheet: What Your Line Actually Needs
Spec sheets are tidy, but real installations rarely are. A cable that meets every listed parameter can still fail early if it can't handle the tight bend behind a machine panel or the constant vibration from a nearby conveyor. Instead of trusting nominal values alone, ask how the line will actually flex, drag, and rub against surrounding surfaces day after day.
Numbers like tensile strength and temperature rating give a false sense of security when they are measured in a lab, not on your floor. The key is to match the cable's mechanical behavior to the motion path it will follow. A highly stiff cable with impressive pull strength might crack under repeated torsion, while a softer jacket could survive for years. What matters is the combination of flexibility, abrasion resistance, and fatigue life in your specific routing, not the headline figure.
Drop the habit of comparing columns on a datasheet and start listing the environmental stresses your line actually produces. Is there cutting fluid mist, metal shavings, or frequent washdowns? Does the cable need to coil and uncoil hundreds of times per shift? Those real-world demands point to jacket materials, shielding styles, and conductor strand counts that no generic specification can dictate. Build the cable around the machine's habits, not the other way around.
Sanitary Design Details That Prevent Costly Recalls
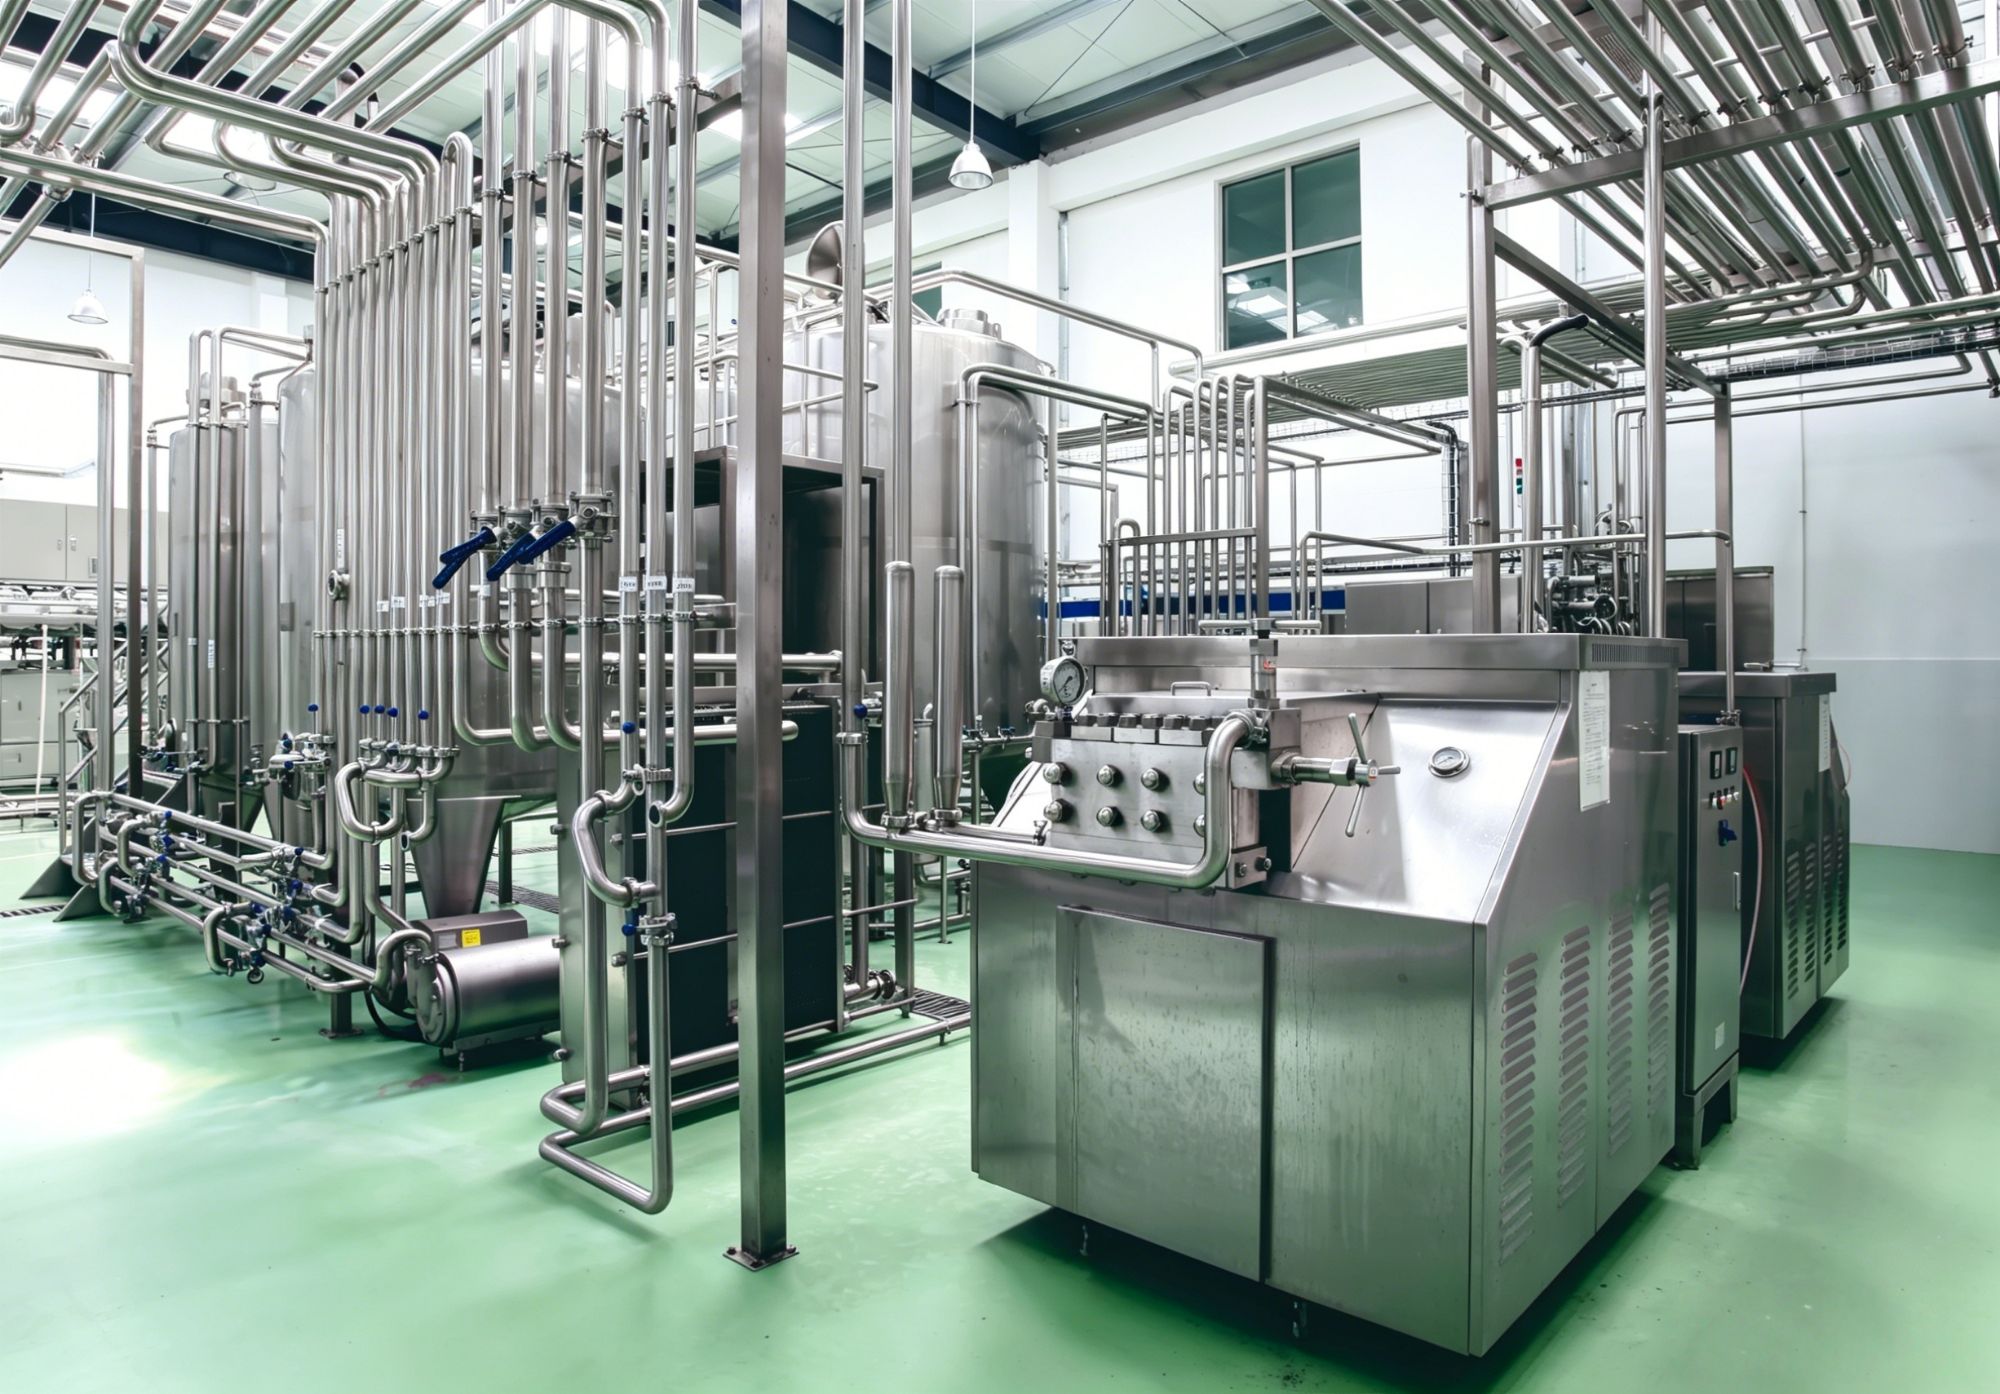
Small gaps, rough welds, and hidden ledges might not look dangerous at first glance, but they give bacteria exactly what they need to survive a cleaning cycle. When moisture and food particles become trapped in these micro-crevices, sanitizers can't reach them, and pathogens multiply out of sight. Over time, a single poorly designed drain or an unpolished corner can turn a whole production line into a recall waiting to happen.
The most effective defenses are built into the equipment itself, long before the first batch runs. Sloped surfaces that shed water instead of pooling it, continuous welds ground flush and polished to a mirror finish, and stand-offs that lift motors and gearboxes away from product zones all remove the places where contamination hides. Even details like the pitch of a pipe or the radius of an internal corner matter: too sharp, and debris collects; too rough, and biofilm clings.
Plants that treat sanitary design as an engineering requirement rather than an afterthought rarely see the nightmare of a market withdrawal. Their lines can be broken down, inspected, and reassembled without leaving a single unreachable shadow zone. That level of confidence doesn't come from more aggressive chemicals or longer wash cycles—it comes from geometry that simply doesn't give bacteria a foothold.
When a Vendor's Track Record Speaks Louder Than a Brochure
In procurement circles, a glossy brochure can promise the moon, but nothing cuts through a room of skeptical engineers like a vendor who quietly lists the three manufacturing lines they kept running through a global chip shortage. Track record isn't just history; it's the residue of decisions made under pressure.
Marketing collateral tends to smooth over the rough edges—the late nights, the scrapped prototypes, the supplier who went dark. A real track record wears those scars openly. When a vendor can point to a failed deployment that they turned around in six weeks, that story does more than any feature matrix. It tells you how they'll behave when your project hits the rocks.
Smart buyers learn to read between the lines of a case study. They ask for the names of the people who were in the room, not just the logos. Because at the end of the day, a brochure is a promise written in ink; a track record is a promise already kept. And in a competitive field, that distinction is the whole game.
The Hidden Costs of a 'Bargain' Bottling Line
The sticker price looks tempting until you unpack the crates. A low-cost bottling line often arrives with thinner gauge stainless, off-spec pneumatics, and control panels that require a specialist just to interpret the error codes. The real expense shows up in the first month when a two-dollar O-ring fails and halts production for six hours while you hunt for a supplier who stocks metric fittings no local distributor carries.
Then there is the quiet drain of inconsistent performance. Cheap fillers drift out of tolerance by mid-shift, underfilling some bottles and overfilling others. That means either giving away product or facing retailer chargebacks. Changeover between bottle sizes, which should take forty minutes, becomes a half-day wrestling match with worn alignment stars and mislabeled HMI menus. Your operators learn to compensate, but every workaround is a small production loss.
Over a two-year span, the savings from that invoice evaporate in air compressor upgrades, emergency service calls, and the overtime needed to hit delivery deadlines. A bargain line often lacks the service network and spare-parts ecosystem that established manufacturers provide, so you end up paying twice: once for the machine and again for the downtime, wasted product, and extra labor it quietly demands.
Questions to Ask About Training, Spare Parts, and Emergency Support
Training questions rarely get past 'Do you offer it?' That leaves your team stuck with a generic slideshow that means nothing on the floor. Ask instead whether the supplier will tailor sessions to your specific equipment configurations, include hands-on practice with your own operators, and provide follow-up refresher access after the initial visit. Also confirm who actually delivers the training—an experienced field engineer or a sales rep reading from a script.
Spare parts conversations often go sideways months later when a critical component fails. Push for a detailed list of recommended spares based on historical failure rates, not just a glossy catalog. Find out where those parts are physically stocked, the realistic lead time for items not on site, and whether the supplier offers consignment stock or automatic replenishment tied to your usage data. If they can't answer those, your downtime will become their education.
Emergency support promises mean nothing without specifics. Ask for the actual on-call roster, not a phone number that rings to voicemail. Inquire about guaranteed response windows, whether remote diagnostics are available for your machine model, and how many certified technicians are within a two-hour drive of your facility. Also clarify what happens when the first fix doesn't work—will the same engineer return, or do you start over with a new case number?
Future-Proofing Your Facility Without Overpaying for Hype
Managers often assume that staying ahead means adopting every new sensor, dashboard, or automation platform that generates buzz. That approach rarely pays off. The real work is in separating durable capabilities from temporary novelty. Look for systems built around open protocols and standard interfaces, because those give you the freedom to swap components later without a full teardown. Modular power distribution, reconfigurable cabling, and scalable network backbones cost more upfront but save multiples down the road.
Another overlooked move is documenting your current loads, failure points, and peak demands before any vendor walks in the door. When you know exactly what your facility consumes and where it strains, you can evaluate new offerings against measured needs instead of marketing claims. Often the smartest future-proofing step is simply leaving spare capacity in conduits, racks, and electrical panels—space that lets you add capacity later without a major retrofit.
Finally, avoid committing to a single vendor's proprietary ecosystem for core infrastructure. The moment you lock into closed protocols or exclusive service contracts, every future upgrade carries a hidden tax. Choose components that can be integrated, monitored, and replaced through standard tools. That way, when a genuinely useful technology emerges, you can adopt it on your own terms and at a reasonable cost.
FAQ
Look beyond glossy brochures and ask for a detailed line layout drawing tailored to your bottle size, product viscosity, and target output. A manufacturer that asks about your CIP requirements and changeover times before quoting is usually thinking about your actual operation, not just selling equipment.
Request a list of installations that match your product category—carbonated soft drinks, dairy, juices, or beer—and then call at least two references. Ask them about foam control during filling, cap torque consistency, and whether the line met uptime guarantees after ramp-up.
A line built around standard modules may force you to adjust your packaging formats or accept slower changeovers. Customization should address your bottle neck diameter, label panel height, and conveyor elevation. The cheapest quote often hides extra costs for retrofits and lost production during suboptimal startups.
Ask about their average response time for a down line, whether they stock critical spares in your region, and if they offer remote diagnostics with a defined escalation path. A partner who gives you a named service engineer and a promised four-hour callback is far more valuable than one with a generic support portal.
It is not just a checkbox. If the manufacturer cannot provide documentation for FDA or EU food contact materials, or does not build to local electrical codes, you may face costly re-inspections and delays. Request the actual certificates and match the serial numbers to the equipment before signing.
Insist on a FAT with your own product, not just water. Run the line at the specified speed for at least four hours, simulate a jam or a missing bottle, and measure actual filler accuracy and label placement. If the manufacturer rushes this step or limits your access, treat it as a red flag.
Compare energy consumption per thousand bottles, spare parts pricing for wear items like grippers and fill valves, and the expected lifespan of motors and drives. Ask for a five-year cost projection that includes maintenance labor, and then verify those numbers with existing customers in a similar climate and shift pattern.
Conclusion
Selecting a beverage production line manufacturer starts with understanding your floor, not just a spec sheet. A line rated for 30,000 bottles per hour means little if your product range demands frequent changeovers or your facility has tight corners and low ceilings. Walk through your current bottlenecks, container formats, and staffing levels before comparing vendors. Then examine sanitary construction closely—polished welds, sloped surfaces, and CIP access matter more than any marketing claim, because a hidden product trap can trigger a recall that erases years of brand trust. Equally important is a vendor's real-world record. Request references from plants running similar products, and if possible visit their lines unannounced. Ask operators about downtime frequency, how fast the manufacturer responded to breakdowns, and whether promised output was actually met. Brochures rarely mention the line that stalled every Friday afternoon.
A low purchase price often hides higher lifetime costs: extra labor for manual adjustments, more frequent replacement parts, higher energy draw, and longer unplanned stops. Before signing, get clear answers on training depth, local spare parts stock, and emergency response windows—not vague guarantees. Ask what happens when a servo fails at 2 a.m. on a holiday weekend, and how quickly a technician actually arrives. Finally, future-proofing should be about practical modularity, not buzzwords. Confirm the control system can accept software updates, that filler heads can be added or changed without a full rebuild, and that any automation you buy solves a real problem today, not a hypothetical one five years from now. A partner who asks hard questions about your operation is worth more than one who promises everything.
Contact Us
Contact Person: Laura
Email: [email protected]
Tel/WhatsApp: +86 13957758832
Website: https://www.intopmachinery.com